Paper I — Q8
(a) The following data represents the results of inspecting 50 units/day of personal computers produced by two processes A and B…
The following data represents the results of inspecting 50 units/day of personal computers produced by two processes A and B of a company for the past ten days.
| Sample No. | Process A No. of Non-Conforming Units | Process B No. of Non-Conforming Units |
|---|---|---|
| 1 | 5 | 8 |
| 2 | 6 | 7 |
| 3 | 7 | 8 |
| 4 | 5 | 9 |
| 5 | 4 | 10 |
| 6 | 6 | 11 |
| 7 | 5 | 15 |
| 8 | 7 | 8 |
| 9 | 9 | 9 |
| 10 | 6 | 7 |
Calculate control limits for both the processes A and B separately and also see if there is need for revision of control limits in any of the processes.
The company claims that 5 PCs may be non-conforming at most out of 50 produced. Perform hypothesis tests for each process using Z-distribution to determine whether the claim of the company is valid for both or not. (Use Normal Distribution table) 20 marks
A medium carbon steel cylindrical rod is being machined under orthogonal cutting condition with an HSS cutting tool having rake angle as 12°.
While machining, following data were recorded : Vertical component of cutting force = 1600 N; Horizontal component of cutting force = 1250 N; Chip thickness ratio = 0·25.
Calculate the following for the above mentioned machining condition : (i) Normal force on the rake face; (ii) Friction force along the rake face; (iii) Resultant cutting force; (iv) Coefficient of friction at chip tool interface; (v) Normal force on the shear plane; (vi) Shear force along the shear plane. 20 marks
A manufacturing company wants to arrange work-centres A, B, C and D, so as to minimize inter-departmental parts handling costs. The flow of parts and existing work-centres layout are shown below :
| From / To | A | B | C | D |
|---|---|---|---|---|
| A | – | 400 | 500 | 50 |
| B | 300 | – | 200 | 0 |
| C | 0 | 0 | – | 700 |
| D | 0 | 0 | 0 | – |
Parts moved between work-centres
Existing layout: A, B, C, D in a row, adjacent centres 30 m apart (A–B, B–C, C–D = 30 m each).
Suggest a modified layout. 10 marks
हिंदी में प्रश्न पढ़ें
निम्नलिखित आँकड़े पिछले 10 दिनों के हैं जो एक कंपनी की दो प्रक्रियाओं A और B द्वारा 50 इकाई प्रतिदिन उत्पादित निजी कंप्यूटर (पी.सी.) के निरीक्षण के परिणामों को दर्शाते हैं :
| नमूना संख्या | प्रक्रिया A गैर-अनुकूलक इकाइयों की संख्या | प्रक्रिया B गैर-अनुकूलक इकाइयों की संख्या |
|---|---|---|
| 1 | 5 | 8 |
| 2 | 6 | 7 |
| 3 | 7 | 8 |
| 4 | 5 | 9 |
| 5 | 4 | 10 |
| 6 | 6 | 11 |
| 7 | 5 | 15 |
| 8 | 7 | 8 |
| 9 | 9 | 9 |
| 10 | 6 | 7 |
दोनों प्रक्रियाओं A और B के लिए अलग-अलग नियंत्रण सीमा परिकलित कीजिए तथा यह भी देखिए कि क्या किसी प्रक्रिया की नियंत्रण सीमा में बदलाव की ज़रूरत है ।
कंपनी यह भी दावा करती है कि ज़्यादा-से-ज़्यादा 50 उत्पादित पी.सी. में 5 गैर-अनुकूलक हो सकते हैं । Z-आबंटन का उपयोग करते हुए प्रत्येक प्रक्रिया के लिए परिकल्पना जाँच कीजिए यह ज्ञात करने के लिए कि कंपनी द्वारा दावा की गई दोनों प्रक्रियाओं के लिए यह सही है या नहीं । (सामान्य वितरण तालिका का प्रयोग कीजिए) (20 अंक)
मध्यम कार्बन इस्पात की बेलनाकार छड़ का मशीन लंबिक कतन अवस्था में HSS कतन औजार से किया गया है जिसका नति कोण 12° है।
मशीन के दौरान निम्नलिखित आंकड़ों को अभिलेखबद्ध किया गया : कतन बल का उद्वर्धर घटक = 1600 N; कतन बल का क्षैतिज घटक = 1250 N; छीलन की मोटाई का अनुपात = 0·25।
उपर्युक्त मशीन अवस्था के लिए निम्नलिखित को ज्ञात कीजिए : (i) नति (रैक) तल के लंबवत कार्यरत बल; (ii) नति (रैक) तल की दिशा में घर्षण बल; (iii) परिणामी कतन बल; (iv) छीलन तथा औजार के अंतराफलक का घर्षण गुणांक; (v) अपरूपण तल के लंबवत कार्यरत बल; (vi) अपरूपण तल के अनुदिश अपरूपण बल। (20 अंक)
एक विनिर्माण कंपनी कार्य-स्टेशन A, B, C तथा D को इस तरह व्यवस्थित करना चाहती है जिससे सामानों की अंतर्विभागीय हस्तांतरण लागत कम हो जाए । सामानों का प्रवाह और मौजूदा कार्य-स्टेशन का खाका नीचे दर्शाया गया है :
| से / तक | A | B | C | D |
|---|---|---|---|---|
| A | – | 400 | 500 | 50 |
| B | 300 | – | 200 | 0 |
| C | 0 | 0 | – | 700 |
| D | 0 | 0 | 0 | – |
सामानों का कार्य-स्टेशन के बीच प्रवाह
मौजूदा खाका: A, B, C, D एक पंक्ति में, आसन्न कार्य-स्टेशनों के बीच 30 m की दूरी (A–B, B–C, C–D प्रत्येक 30 m)।
संशोधित खाका का सुझाव दीजिए । (10 अंक)
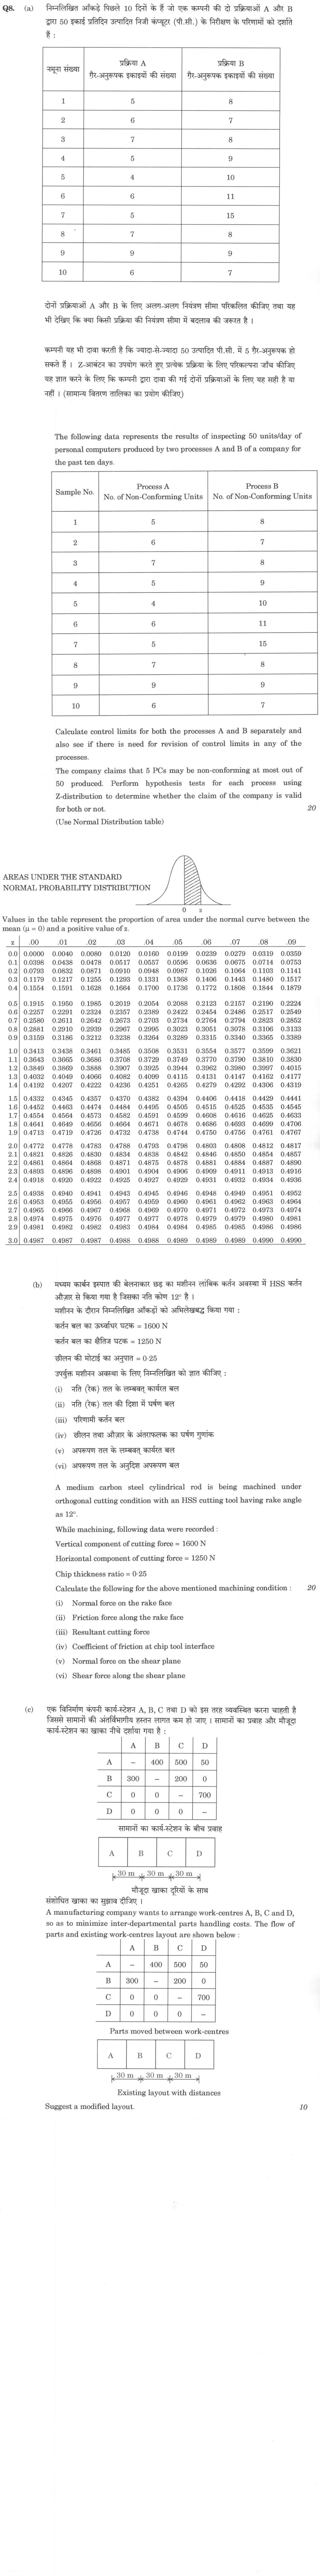
The figure this question refers to, in words
The question paper is a scan and the diagram did not survive as text. This is the figure as read from the original page — every component, value and label — so the question can be worked from the text below.
(a) Table with columns: Sample No., Process A No. of Non-Conforming Units, Process B No. of Non-Conforming Units. Rows: 1, 5, 8; 2, 6, 7; 3, 7, 8; 4, 5, 9; 5, 4, 10; 6, 6, 11; 7, 5, 15; 8, 7, 8; 9, 9, 9; 10, 6, 7.
(b) Text data: Rake angle = 12 degrees. Vertical component of cutting force = 1600 N. Horizontal component of cutting force = 1250 N. Chip thickness ratio = 0.25.
(c) Diagram titled 'Existing layout with distances'. It shows four rectangular blocks arranged in a horizontal line, labeled from left to right as A, B, C, D. Below the blocks, dimension lines indicate the distance between the center of A and B is 30 m, between B and C is 30 m, and between C and D is 30 m.
Model answer
Drafted with AI by UPSC Answer Check against this question's marking rubric, to the expected length. UPSC does not publish answers for Mains — this is one way to score well, not an official key. How we build rubrics and answers.
(a) p-chart control limits and hypothesis test of the company's claim
Each sample has n = 50 PCs, and there are k = 10 samples. The p-chart is used, with 3-sigma limits.
Process A: total non-conforming = 5 + 6 + 7 + 5 + 4 + 6 + 5 + 7 + 9 + 6 = 60. p̄ = 60/500 = 0.12, σ_p = √(0.12 × 0.88/50) = 0.0460. UCL = 0.12 + 3(0.0460) = 0.258; LCL = 0.12 − 0.138 = −0.018, taken as 0. The largest sample proportion is 9/50 = 0.18, below the UCL, and none is below the LCL. Process A is in control.
Process B: total non-conforming = 8 + 7 + 8 + 9 + 10 + 11 + 15 + 8 + 9 + 7 = 92. p̄ = 92/500 = 0.184, σ_p = √(0.184 × 0.816/50) = 0.0548. UCL = 0.184 + 0.164 = 0.348; LCL = 0.184 − 0.164 = 0.020. The sample proportions run from 7/50 = 0.14 to 15/50 = 0.30 (sample 7), all inside 0.020–0.348. Process B is also in control. No point lies outside the limits, so neither process needs its limits revised.
Hypothesis test. The claim "at most 5 non-conforming in 50" means p ≤ 0.10. H₀: p ≤ 0.10, H₁: p > 0.10 (one-tailed), α = 0.05, critical Z = 1.645 (table area 0.45). Standard error with all 500 PCs: √(0.10 × 0.90/500) = 0.01342. Process A: Z = (0.12 − 0.10)/0.01342 = 1.49 < 1.645. H₀ is not rejected, so the claim is acceptable for A (table area 0.4319 gives p ≈ 0.068, above 0.05). Process B: Z = (0.184 − 0.10)/0.01342 = 6.26 > 1.645. H₀ is rejected, so the claim is not valid for B. The claim is therefore valid for A but not for B, and not for both.
(b) Orthogonal cutting forces and friction
Data: α = 12°, cutting force (vertical) F_c = 1600 N, thrust force (horizontal) F_t = 1250 N, chip thickness ratio r = 0.25.
(i) Normal force on the rake face: N = F_c cosα − F_t sinα = 1600(0.9781) − 1250(0.2079) = 1565.0 − 259.9 = 1305 N. (ii) Friction force on the rake face: F = F_c sinα + F_t cosα = 332.7 + 1222.7 = 1555 N. (iii) Resultant force: R = √(1600² + 1250²) = 2030 N, which also equals √(N² + F²). (iv) Coefficient of friction: μ = F/N = 1555/1305 = 1.19. Shear angle: tanφ = r cosα/(1 − r sinα) = 0.2445/0.9480 = 0.2579, so φ = 14.46°. (v) Normal force on the shear plane: N_s = F_c sinφ + F_t cosφ = 399.7 + 1210.3 = 1610 N. (vi) Shear force on the shear plane: F_s = F_c cosφ − F_t sinφ = 1549.3 − 312.2 = 1237 N.
Check: √(1610² + 1237²) = 2030 N, equal to R.
(c) Modified layout to reduce handling cost
Combine the flows in both directions between each pair: A–B = 400 + 300 = 700; A–C = 500; A–D = 50; B–C = 200; C–D = 700; B–D = 0.
Existing layout A-B-C-D (30 m spacing). Handling cost measured as flow × distance in units of 30 m: A–B 700 × 1 = 700; A–C 500 × 2 = 1000; A–D 50 × 3 = 150; B–C 200 × 1 = 200; C–D 700 × 1 = 700. Total = 2750 (82 500 part-metres).
The two heaviest flows are A–B and C–D (700 each), then A–C (500). Place A–B adjacent, C–D adjacent, and bring A next to C. This gives the layout B-A-C-D: A–B 700 × 1 = 700; A–C 500 × 1 = 500; A–D 50 × 2 = 100; B–C 200 × 2 = 400; C–D 700 × 1 = 700. Total = 2400 (72 000 part-metres).
Trying all 24 linear arrangements, B-A-C-D (and its mirror D-C-A-B) gives the minimum. The modified layout B-A-C-D reduces handling by 350 units of 30 m, about 12.7%, simply by interchanging A and B.

How this answer will be evaluated
Framework: null
What earns full marks: All calculations correct, clear reasoning, and well-justified layout.
Evaluation rubric
Each sub-part is marked on its own, against the marks and word limit printed on the paper.
- (a) Compute p-chart control limits for processes A and B, check for revision, and test the claim of at most 5 non-conforming in 50. 20 marks
calculate— given → formula → substitution → result with units → interpretation
Must cover
- A: p-bar 0.12, UCL 0.258, LCL 0; B: p-bar 0.184, UCL 0.348, LCL 0.020
- Both processes in control, no revision
- H0 p <= 0.10 one-tailed, critical Z 1.645
- Z_A 1.49 not rejected; Z_B 6.26 rejected
Loses marks
- Using a two-tailed test.
Earns more
- Marks for limits, control check, hypotheses, Z values and conclusions.
Extra mark
- P-value from the normal table.
- (b) Calculate the rake-face forces, friction coefficient, resultant and shear-plane forces in orthogonal cutting. 20 marks
calculate— given → formula → substitution → result with units → interpretation
Must cover
- N = 1305 N and F = 1555 N
- Resultant 2030 N and mu 1.19
- Shear angle 14.46 degrees
- N_s 1610 N and F_s 1237 N
Loses marks
- Swapping the cutting and thrust forces.
Earns more
- Marks for rake-face forces, resultant, mu, shear angle and shear-plane forces.
Extra mark
- Resultant check from both components.
- (c) Suggest a modified layout of work-centres A to D to reduce handling cost. 10 marks
suggest— the problem in one line → implementable measures → who acts → conclusion
Must cover
- Combine bidirectional flows A-B 700, A-C 500, C-D 700
- Existing cost 2750 units
- Modified layout B-A-C-D cost 2400
- About 12.7 percent saving
Loses marks
- Ignoring the B to A flow.
Earns more
- Marks for combined flows, cost of existing layout, modified layout and saving.
Extra mark
- Evidence of trying other arrangements.
What "Calculate" is asking you to do
Apply the standard formula or schedule to data the question has already supplied — a table of readings, cost records, a balance sheet — and produce the number. The method is rarely in doubt; the marks sit in the named intermediate quantities, each of which has to appear as a labelled line.
Structure that answers it
Data as given → formula or standard treatment, named → substitution → each intermediate, labelled → result with units
Where marks are lost
Omitting an intermediate the marking scheme pays for separately, or rounding at an intermediate line so the final figure drifts. In commerce and accountancy, any figure in a statement that no numbered working note supports is treated as unearned.
Practice this exact question
Write your answer and it is marked point by point against the model answer above — what you covered, what you missed, what you got wrong.
Evaluate my answer →More from Mechanical Engineering 2023 Paper I
- Q5 (a) In an electrochemical machining process of an iron surface using sodium chloride solu…
- Q6 (a) Following data were observed while machining two different work materials X and Y usi…
- Q7 (a) (i) A tube is to be drawn as per the dimensions given in the following Figure 7(a)(i)…
- Q8 (a) The following data represents the results of inspecting 50 units/day of personal comp…